
Views: 0 Author: Site Editor Publish Time: 2026-10-12 Origin: Site


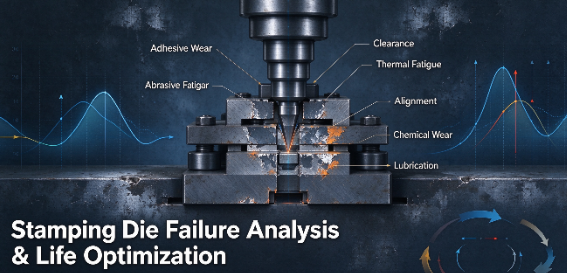
Unplanned tooling maintenance and high scrap rates destroy margins in high-volume manufacturing. These issues usually trace back to a single failure point: compromised tooling integrity. While gradual tool degradation happens naturally over millions of cycles, premature stamping die wear disrupts production schedules, inflates cost-per-part, and forces reactive emergency repairs. Moving from reactive firefighting to proactive prevention requires a systematic evaluation of wear mechanisms. You must analyze tool steel metallurgy, press alignment, and lubrication chemistry to determine the most effective intervention. Manufacturers cannot rely on visual inspections alone to gauge tool health. Modern production demands a rigorous understanding of the physics happening inside the press. By diagnosing the exact mode of failure, engineers implement targeted solutions that extend tool life, improve part quality, and stabilize production output.
Identify the Wear Mechanism First: Distinguishing between adhesive wear (galling), abrasive wear, thermal fatigue, and mechanical fatigue is critical before investing in tooling modifications or new coatings.
Material and Substrate Mismatch is a Primary Culprit: The rise of Advanced High-Strength Steels (AHSS) frequently overpowers legacy tool steels, necessitating upgraded die materials or advanced Surface Engineered Coatings (PVD/CVD).
Lubrication and Alignment Dictate ROI: Even premium tool steels will fail prematurely if press deflection, improper die clearance, or inadequate boundary lubrication are present.
Predictive Maintenance Outperforms Scheduled Maintenance: Integrating tonnage monitors, in-die sensors, and Computerized Maintenance Management Systems (CMMS) shifts the maintenance paradigm from reactive to predictive, maximizing the stamping die lifecycle.
Table of Contents
Stamping mold wear affects more than repair costs. Frequent tooling failures increase downtime, scrap rates, and maintenance expenses. Establishing measurable performance benchmarks helps manufacturers control costs and improve die service life.
Cost Type | Key Expenses |
|---|---|
Direct Costs | Punch replacement, die repair, EDM machining, maintenance labor |
Indirect Costs | Production downtime, rejected parts, quality inspection, delayed deliveries |
Indirect costs can significantly increase the total financial impact of premature tooling wear.
Manufacturers should monitor the following indicators:
Hits per Sharpening: Stamping cycles between sharpening operations.
Tooling Cost per Part: Total tooling expenses divided by acceptable parts produced.
Scrap Rate: Percentage of rejected stamped components.
Downtime: Production hours lost due to tooling maintenance.
Tool Life: Total strokes before component replacement.
Check Material Properties: Verify sheet thickness and tensile strength.
Evaluate Tool Steel: Confirm steel grade and surface hardness.
Optimize Die Clearance: Match cutting clearance to material requirements.
Set Maintenance Targets: Use historical stroke counts and tooling performance data.
Tooling Condition | Recommended Action |
|---|---|
Minor edge wear | Sharpen and inspect |
Frequent galling or abrasion | Improve lubrication or upgrade coatings |
Repeated punch damage | Check alignment, clearance, and tool materials |
Persistent failures and high downtime | Consider die redesign or replacement |
The goal is to minimize tooling cost per acceptable part, rather than focusing only on individual repair expenses.

Premature stamping mold wear results from friction, mechanical stress, temperature fluctuations, and chemical reactions. Identifying the specific wear mechanism helps manufacturers select suitable tooling materials, coatings, lubrication, and maintenance strategies to extend die service life.

Adhesive wear occurs when high pressure and friction cause sheet metal to bond to the stamping die surface. This material transfer creates scratches, increases stripping force, and accelerates tooling damage. Proper lubrication, compatible surface coatings, and optimized forming conditions help reduce galling and improve die durability.
Abrasive wear develops when hard particles, metal debris, or surface scale scratch and remove material from tooling surfaces. Common symptoms include parallel grooves, dull cutting edges, and dimensional inaccuracies. Maintaining clean sheet metal surfaces and selecting wear-resistant tool steels or coatings helps minimize abrasive damage.
Surface fatigue results from repeated stamping loads that gradually create microscopic cracks in tool steel. These cracks can develop into edge chipping, surface spalling, or punch breakage. Proper heat treatment, balanced hardness and toughness, and controlled loading help prevent premature fatigue failure.
Thermal fatigue occurs when repeated heating and cooling cause expansion and contraction of stamping die surfaces. This can produce fine surface cracks, known as heat checking, which may lead to material loss over time. Optimizing stamping speed, lubrication, cooling, and tool material selection helps reduce thermal stress.
Corrosive wear occurs when incompatible lubricants, additives, or processing chemicals react with tooling materials. Certain chemical formulations may damage tool steel surfaces or carbide binders, reducing wear resistance and service life. Selecting chemically compatible lubricants and tool materials helps prevent corrosion-related failures.
Wear Mechanism | Visual Symptom on Part/Tool | Immediate Shop-Floor Check |
|---|---|---|
Adhesive Wear (Galling) | Deep scoring on drawn parts, material buildup on punch | Verify lubricant concentration and spray nozzle alignment |
Abrasive Wear (Scoring) | Parallel grooves on die surface, rapid dimensional loss | Inspect incoming coil for heavy mill scale or slitting burrs |
Surface Fatigue (Chipping) | Missing fragments on cutting edges, sudden burr increase | Check tool steel hardness (HRC) and verify press parallelism |
Thermal Fatigue (Heat Checking) | Spiderweb-like micro-cracks on the tool surface | Monitor tool operating temperature and adjust press speed |
Identifying the wear mechanism provides the symptoms, but engineers must dig deeper to find the root causes. Premature failure usually stems from a disconnect between the tool's design parameters and the reality of the production floor.
Selecting the right tool steel requires balancing toughness against wear resistance. Legacy materials like D2 offer decent baseline performance for mild steels, but they frequently fail when tasked with forming modern, high-strength alloys. Transitioning to powder metallurgy (PM) steels like CPM-10V or utilizing solid carbide inserts provides the necessary vanadium or tungsten carbides to resist severe abrasion. The uniform carbide distribution in PM steels prevents the large carbide pooling that often leads to chipping in conventional ingot steels.
Even the most advanced PM steel will fail if the heat treatment is flawed. Decarburization during the hardening process leaves a soft outer skin that wears away instantly. Conversely, insufficient tempering leaves the core brittle and prone to shattering under load. Strict adherence to metallurgical specifications, including proper austenitizing temperatures and multiple tempering cycles, is non-negotiable for a healthy Stamping Die.
Press misalignment and excessive deflection can cause uneven die clearance, premature punch wear, and tooling damage. Worn guide systems, off-center loading, and insufficient frame rigidity affect ram-to-bed parallelism. Regular press inspections, gib adjustments, and dynamic alignment checks help maintain stamping accuracy and extend tooling life.
Slug pulling occurs when punched scrap returns to the die surface instead of falling away, potentially damaging punches and die components during the next stroke. Common causes include suction, excessive lubrication, and residual magnetism. Proper die geometry, ejector pins, and suitable scrap removal systems help prevent slug pulling and maintain stable production.
Improper stamping lubrication increases friction, heat, and galling, accelerating die wear. Lubricants must match the workpiece material and forming requirements, particularly for high-strength steels and deep drawing operations. Consistent lubricant application and regular nozzle inspections help prevent dry spots, improve forming quality, and reduce tooling damage.
Sheet metal variations in thickness, hardness, and surface condition can affect cutting clearance and tooling performance. High-strength materials such as AHSS require greater forming forces and suitable die designs. Monitoring incoming material quality and adjusting tooling specifications help reduce unexpected wear, dimensional defects, and production interruptions.
Preventing premature stamping die wear requires a combination of material upgrades, mechanical optimization, automated monitoring, and preventive maintenance. Addressing the underlying causes helps improve tooling reliability and reduce long-term production costs.
Advanced tool steels and surface coatings improve wear resistance and reduce friction in demanding stamping applications. Powder metallurgy steels and tungsten carbide provide enhanced durability for suitable operating conditions, while PVD, CVD, and TD coatings help minimize galling and surface damage. Proper material and coating selection can extend tool life and reduce sharpening frequency.
Correct die clearance and press alignment are essential for consistent stamping performance. Engineers should adjust punch-to-die clearance according to material thickness, strength, and cutting requirements. Regular inspections of ram parallelism, guide systems, and press rigidity help prevent uneven loading, excessive burrs, and premature tooling failure.
Automated lubrication systems provide consistent lubricant distribution, reducing friction and preventing dry contact during stamping. In-die sensors and tonnage monitoring systems can detect abnormal forces, misfeeds, and slug pulling before major damage occurs. These technologies improve process stability, minimize material waste, and reduce unexpected downtime.
Computerized Maintenance Management Systems (CMMS) help manufacturers track stamping cycles, maintenance schedules, component replacements, and tooling failures. Historical performance data supports preventive maintenance planning and identifies recurring wear problems. This data-driven approach improves equipment reliability, extends die service life, and reduces maintenance costs.
Pull historical scrap and downtime data to identify the three highest-maintenance dies currently running in your facility.
Conduct a dynamic press alignment check to measure ram parallelism and gib clearance under actual stamping tonnage.
Audit your current lubrication application system to identify clogged nozzles, inconsistent spray patterns, or incorrect fluid viscosity.
Verify that your cutting clearances match the specific shear strength and thickness of the incoming coil material.
Implement a strict stroke-count tracking system to schedule preventative sharpening before catastrophic edge failure occurs.
A: The acceptable lifespan varies heavily based on the material being stamped and the tool steel used. A die cutting standard mild steel might achieve 500,000 to 1,000,000 strokes between sharpenings. However, stamping Advanced High-Strength Steels (AHSS) can reduce that lifespan to 50,000 strokes without specialized coatings or powder metallurgy tool steels.
A: Improper die clearance forces the tool to work harder. If clearance is too tight, friction increases exponentially, leading to rapid abrasive wear and galling. If clearance is too loose, the material bends before tearing, creating heavy burrs and increasing the risk of slug pulling. Optimal clearance distributes cutting forces evenly.
A: Galling itself is a symptom, not the root cause. While operators can polish away the micro-welded material to restore the surface temporarily, galling will return unless the underlying issue is fixed. Permanent prevention requires upgrading the lubricant chemistry, applying anti-friction surface coatings, or changing the tool steel grade.
A: There is no single best coating; it depends on the failure mode. Titanium Nitride (TiN) provides good general-purpose wear resistance. Titanium Carbonitride (TiCN) is excellent for abrasive environments. For severe forming and deep drawing operations prone to galling, Thermal Diffusion (TD) or Chemical Vapor Deposition (CVD) coatings offer superior protection.
A: Slug pulling draws punched scrap back onto the die surface. When the press cycles again, the hardened punch crushes the scrap piece directly into the die block. This localized, extreme pressure causes immediate catastrophic damage, frequently chipping the die edge or entirely shattering the punch.
A: Yes, many PVD and CVD coatings can be chemically stripped and reapplied after the tool is sharpened. However, repeated stripping cycles can degrade the surface integrity of the underlying tool steel substrate, potentially leading to hydrogen embrittlement or microscopic dimensional changes over time.


