
Views: 0 Author: Site Editor Publish Time: 2026-10-12 Origin: Site


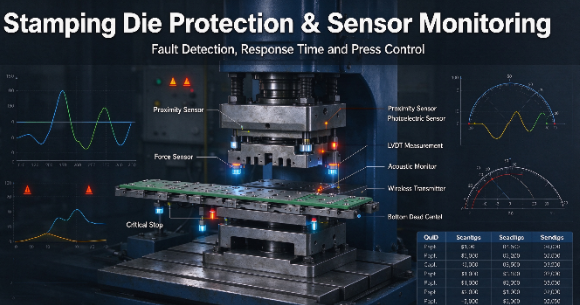
A catastrophic die smash in high-speed stamping or cold forming operations carries a compounding financial impact. Direct tooling repair costs, scrapped materials, and unplanned production downtime can cripple a manufacturing run. Modern press speeds far exceed human reaction times. Manual monitoring simply cannot detect misfeeds, slug stacking, or part ejection failures before the press ram reaches Bottom Dead Center (BDC). Operators cannot hit the emergency stop fast enough to prevent a crash. Relying on visual inspection leaves expensive progressive dies entirely vulnerable to unpredictable mechanical anomalies.
Integrating a reliable die protection sensor network automates fault detection. This setup halts the press instantly when anomalies occur. It transitions operations from reactive maintenance to intelligent, adaptive process control via computerized feedback. By monitoring the internal mechanics of the tool during every single stroke, manufacturers protect their equipment and ensure consistent part quality.
Failure-Specific Matching: Selecting the correct die protection sensors requires mapping sensor technologies (inductive, photoelectric, force, measurement) to specific failure modes like short feeds, long feeds, or failure to eject.
Response Time is Critical: Sensor efficacy is dictated by the press control system's ability to process the signal and engage the clutch/brake mechanism before the die closes on a fault.
Environmental Survivability: Stamping environments destroy fragile electronics; evaluating sensors based on shock, vibration, and cutting fluid resistance is as important as sensing accuracy.
Wired vs. Wireless Trade-offs: Advancements in wireless transmitter systems are resolving traditional failure points caused by wire fatigue and vibration in high-speed tooling, drastically reducing downtime.
Table of Contents
A successful die protection program must achieve zero catastrophic die smashes while minimizing false stops. Frequent false stops, known as nuisance tripping, severely degrade Overall Equipment Effectiveness (OEE). When nuisance tripping becomes excessive, operators frequently bypass safety systems to maintain production quotas. Balancing detection sensitivity with operational reliability remains the core objective of any sensor integration project on the stamping floor.
Understanding exactly how dies fail allows engineering teams to select the right detection method. Different mechanical issues present distinct physical signatures during the press cycle. A 200-ton press running at 150 Strokes Per Minute (SPM) carries immense kinetic energy. When that energy meets an obstruction, the weakest point in the mechanical chain fails instantly.
Misfeeds (Short and Long): Material fails to advance to the precise progression length. Coil binding, feeder slippage, or improper pilot release timing causes short feeds. Long feeds happen when momentum carries the strip too far past the intended station. If a 0.060-inch steel strip misfeeds by just a quarter of an inch, the pilot punches strike solid material instead of the pre-punched pilot holes. The force required to pierce that solid material exceeds the punch's design limits, causing the tool steel to shatter.
Slug Pulling and Stacking: Scrap material fails to clear the die block after a piercing operation. A vacuum effect or highly viscous drawing lubricants can pull the slug back up to the die surface as the punch retracts. Subsequent strokes compress multiple slugs together. This creates extreme localized pressure that easily cracks die matrices or snaps punches.
Part Ejection Failures: Finished parts remain trapped in the die cavity during the next stroke. Pneumatic air ejectors might fail, or parts might stick to the punch due to heavy oil adhesion. Stamping a new part directly on top of an un-ejected part guarantees severe tool damage and potential damage to the press crankshaft.
Dimensional Drift: Gradual tooling wear leads to out-of-tolerance parts over long production runs. Thermal expansion during high-speed stamping also shifts critical dimensions. In-die measurement sensors catch this drift during the production run rather than at final quality inspection, preventing massive scrap sorting efforts.

Operating without in-die monitoring exposes equipment to severe mechanical risks. Rebuilding complex progressive dies requires weeks of specialized labor from highly skilled toolmakers. Repairing a damaged press crankshaft or replacing a bent pitman arm requires heavy rigging, specialized machining, and extended downtime. The kinetic energy from a severe crash transfers back up through the ram, scoring crankshaft bearings and misaligning the press frame. Relying on luck or operator reflexes is not a sustainable manufacturing strategy.
No single sensor type catches every fault. Tooling engineers must build a network of specialized devices tailored to the specific actions happening inside the tool. Each technology has distinct strengths, optimal target materials, and environmental limitations.
Inductive sensors detect metallic objects using oscillating electromagnetic fields. When a metal target enters the field, eddy currents draw energy away from the oscillator, dropping the amplitude and triggering the sensor output. They are highly reliable in dirty environments because they completely ignore non-metallic contaminants like heavy stamping oil, water, and synthetic lubricants. Toolmakers use them to confirm stripper plate position, verify pilot pin insertion, or ensure the material strip sits flat on the die block. Their solid-state construction makes them highly resistant to the continuous vibration of a stamping press.
Capacitive sensors detect non-metallic materials by measuring changes in dielectric properties. They work well for detecting plastic components or monitoring fluid levels in automated die lubrication systems. However, capacitive sensors are highly sensitive to moisture and heavy oil buildup. In aggressive stamping environments, ambient oil mist can coat the sensor face and cause false readings, making them less ideal for direct in-die part detection.
Through-beam and retroreflective sensors excel at part ejection verification. They project a concentrated beam of light across the ejection path. When an air-ejected part breaks the light curtain, the sensor sends a rapid confirmation signal to the press control. Fiber optic variants allow toolmakers to route the sensing heads into extremely tight spaces within the die shoe, keeping the fragile electronics safely mounted outside the strike zone.
Heavy oil mist and flying metal debris easily foul optical lenses. This requires regular maintenance and dedicated air-purge systems to keep the lenses clean during operation. If the lens gets dirty, the sensor fails to register the light beam, causing a false stop. You must position optical sensors carefully to minimize exposure to direct fluid spray and high-pressure air blasts.
Force sensors, typically utilizing piezoelectric load cells, sit within or beneath individual tool stations. You place them directly under coining, bending, staking, and hole piercing stations. They measure the dynamic force exerted during the working portion of the stroke. By capturing the unique force signature of a good part, the system establishes a baseline force curve.
These sensors detect sudden tonnage spikes instantly. A spike indicates slug stacking, dull punches, or variations in incoming material thickness. Catching a localized overload prevents catastrophic failure before the die block fractures. They provide a much higher resolution than standard press tonnage monitors, which only measure the total ram force and often miss small, localized overloads in a large progressive die.
Precision measurement sensors provide real-time dimensional verification inside the tool. Linear Variable Differential Transformers (LVDTs) or laser displacement sensors measure flange lengths, hole locations, or form depths while the part is still attached to the carrier strip. They utilize computerized feedback to detect micro-faults and material variations stroke by stroke.
This catches errors before they cause tool damage or produce scrap. If a bending station starts drifting out of tolerance due to thermal expansion of the tool steel, the measurement sensor alerts the operator immediately. This eliminates the need to quarantine and sort thousands of parts after a long production run completes.
Acoustic sensors detect the specific sound signatures of mechanical events. A misfeed, a broken punch, or a shattered die button creates a distinct high-frequency acoustic emission. These sensors clamp directly onto the die shoe and listen for these anomalies during the working portion of the stroke.
They act as a secondary diagnostic layer, adding redundancy to your primary Die Protection Sensors. Acoustic monitoring is particularly useful for detecting micro-fractures in carbide tooling before the punch completely disintegrates. The system compares the acoustic profile of each stroke against a known good baseline, halting the press if the sound signature deviates.

Selecting the right hardware is only half the battle. You must evaluate how the sensor interacts with the press dynamics and the control architecture. Speed, timing, and environmental ruggedness dictate system success on the shop floor.
Press speed (SPM) and stopping angle determine how quickly sensors must detect faults and trigger a safe stop. High-speed presses require faster response times and precise timing calculations to prevent die damage. Engineers should evaluate sensor detection points, controller response time, and actual braking performance to ensure the press can stop before a collision occurs.
Fixed-limit sensors use preset detection thresholds for basic functions such as part ejection and material positioning. Intelligent adaptive systems monitor force and timing patterns, automatically adjusting detection thresholds to accommodate normal process variations. These systems can reduce false alarms while maintaining reliable die protection.
Stamping sensors must withstand continuous vibration, mechanical shock, lubricants, and harsh industrial conditions. Rugged housings, suitable IP protection ratings, and shock-resistant electronics help prevent premature sensor failure. Selecting sensors designed for metal stamping applications improves monitoring reliability and reduces maintenance downtime.
Sensor Technology |
Target Material |
Primary Stamping Application |
Environmental Resistance |
Typical Response Time |
|---|---|---|---|---|
Inductive Proximity |
Metals Only (Steel, Aluminum, Copper) |
Pilot verification, stripper plate position, short feed detection |
Excellent (Ignores heavy oil, water, and non-metallic dirt) |
< 1 ms |
Photoelectric (Through-Beam) |
Any Solid Object |
Part ejection verification, light curtains, cam return checks |
Poor (Lenses easily fouled by oil mist and flying debris) |
1 - 5 ms |
Piezoelectric Force |
Mechanical Load / Stress |
Slug stacking, dull punch detection, material thickness variation |
Very Good (Requires highly rigid mounting and clean pockets) |
< 0.5 ms |
LVDT Measurement |
Physical Contact |
Dimensional drift, form depth verification, flange length |
Good (Needs physical protection from direct scrap impact) |
2 - 10 ms |
Acoustic Emission |
High-Frequency Sound Waves |
Tool fracture, micro-cracks in carbide, severe galling |
Excellent (Clamped securely to the exterior die shoe) |
< 0.1 ms |
A perfectly selected sensor will fail if installed incorrectly. Mechanical interference, wire routing, and control integration present significant hurdles on the shop floor. Proper implementation requires collaboration between toolmakers, controls engineers, and press operators to ensure the system survives daily production rigors.
Proper sensor placement ensures accurate detection and prevents damage during stamping. Sensors should be recessed into protected die pockets, away from moving components and flying scrap. Maintaining the correct sensing distance and accounting for die vibration and strip movement help improve monitoring accuracy and reliability.
Sensitive die sensors require careful installation to prevent mechanical damage and inaccurate readings. Use clean mounting surfaces, follow manufacturer torque specifications, and protect wiring during assembly. Testing sensors before installing the die in the press helps identify potential faults and ensures reliable operation.
Reliable wiring and connectivity are essential for maintaining die protection system performance. Industrial-grade cables and protected connectors help prevent damage from vibration and frequent die changes. Wireless sensor systems can simplify installation, reduce cable-related failures, and improve changeover efficiency when properly configured.
Die protection sensors integrate with PLCs or dedicated monitoring controllers to detect abnormal conditions and trigger press stops. High-speed stamping applications may require specialized processing modules for rapid response. Programmable timing windows synchronize sensor detection with the press stroke, reducing false alarms and improving operational safety.
In-die sensor systems help reduce tooling damage, production downtime, and material waste by detecting misfeeds, slug pulling, and other stamping abnormalities. Early fault detection protects expensive dies and improves equipment availability. Reliable monitoring also supports automated production, helping manufacturers increase productivity and reduce long-term operating costs.
Audit your top three highest-maintenance progressive dies to identify the most frequent mechanical failure points.
Map the exact stopping time and critical angle of your press using a dedicated stopping time monitor.
Install a pilot sensor array on a single problematic tool station to test environmental survivability and response times.
Upgrade your press control interface to support programmable cam switches for precise sensor interrogation windows.
A: A die protection sensor detects specific mechanical events like misfeeds, part ejection, or component position using proximity or optical technology. A tonnage monitor measures the total force exerted by the press during the stroke to ensure it stays within safe operating limits. Sensors catch localized faults before they affect total tonnage.
A: Response time depends on the press speed (SPM) and the braking mechanism. You must calculate the time it takes for the sensor to detect a fault, signal the controller, and engage the brake before the ram reaches the critical stopping angle where die damage occurs.
A: Yes. Modern wireless transmitter systems are specifically designed for high-impact environments. By eliminating physical cables, they actually resolve traditional failure points caused by wire fatigue and continuous stamping vibration, making them highly reliable.
A: You should mount in-die force sensors directly within or immediately beneath the individual tool station. Placing them directly under the specific punch or die button ensures they capture localized tonnage spikes accurately without interference from other operations.
A: Sensors monitor the die block to ensure scrap material clears the area after each stroke. If a slug pulls back up and stacks, the sensor detects the anomaly or the resulting pressure spike and halts the press instantly before the next stroke crushes the die.
A: A programmable limit switch, or resolver, defines the specific timing windows during the press stroke when a sensor should be monitored or ignored. This prevents false stops during normal events, such as ignoring an optical sensor while the tool physically blocks it during stamping.


