
Views: 0 Author: Site Editor Publish Time: 2026-10-12 Origin: Site


Industrial press selection carries massive stakes for manufacturing facilities. Underspecifying equipment inevitably leads to catastrophic die damage and halted production lines. Standard single-point or two-point presses hit mechanical limits when scaling up production. Large-panel stamping, progressive dies, and asymmetrical parts generate severe off-center loads. Basic machines simply cannot handle these eccentric forces without compromising part quality. Upgrading to a four-point mechanical press represents a strict geometric and kinematic necessity for specific manufacturing profiles. Facilities must evaluate technical fit, facility readiness, and vendor capabilities before committing to this equipment. This guide explores exactly when a factory must transition to four-point suspension to maintain precision, protect tooling, and ensure long-term production stability.
Off-Center Load Mastery: A four-point mechanical press is mandatory when stamping large, asymmetrical parts where uneven force distribution would cause slide tipping in two-point systems.
Die Life Extension: By maintaining strict slide parallelism across massive bed sizes, four-point presses drastically reduce tool wear and maintenance downtime.
Material Capabilities: Essential for forming Advanced High-Strength Steels (AHSS) and aluminum alloys that require high tonnage distributed over a wide area to control springback.
Implementation Reality: The transition requires significant facility preparation, including specialized foundation pits, increased overhead clearance, and upgraded automation integration.
Procurement Strategy: Evaluating new versus rebuilt options and assessing OEM service networks are just as critical as the press's technical specifications.
Table of Contents
Press kinematics dictate how force transfers from the drive mechanism to the tooling. A two-point press utilizes two suspension points, or pitmans, connected to the slide. This design works well for symmetrical loads centered under the ram. However, a Four-Point Mechanical Press utilizes four distinct suspension points positioned near the corners of the slide. This geometric arrangement fundamentally changes how the machine distributes force. The physics of load distribution across four corners ensures that the slide remains parallel to the bolster plate throughout the entire stroke. When stamping forces push back against the ram, the four pitmans resist deflection evenly. This multi-point suspension creates a rigid, stable platform capable of handling massive tonnage across expansive bed areas. The kinetic energy transfers uniformly, preventing the slide from shifting laterally under heavy load.
Two-point mechanical presses may experience slide tipping under excessive off-center loads, causing uneven force distribution, die misalignment, and premature tooling wear. These issues can lead to damaged punches, inconsistent part dimensions, and increased maintenance costs. Four-point presses provide better load distribution and slide stability, reducing tipping risks in large-die and high-tonnage stamping applications.
Tie-rod press frames use preloaded steel rods to connect the crown, uprights, and bed, providing high structural rigidity and controlled frame deformation under heavy loads. Welded frames offer flexible construction and can provide reliable performance when properly engineered. Frame selection depends on tonnage, stiffness requirements, manufacturing costs, and precision needs, with tie-rod designs commonly used in large, heavy-duty stamping presses.
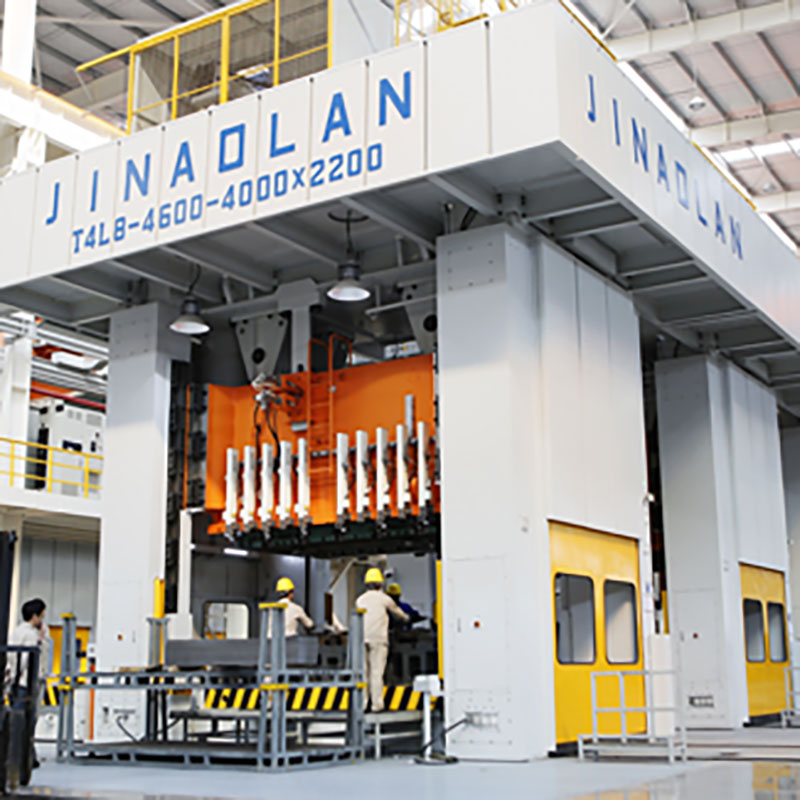
Bed size serves as the primary indicator for four-point suspension requirements. When a bed exceeds 120 to 144 inches left-to-right, or requires deep front-to-back dimensions, four-point suspension becomes non-negotiable. Two pitmans simply cannot support the span of a massive slide without allowing the center or edges to deflect. Large bed sizes are mandatory for multi-station progressive dies and large transfer dies. Automotive body panels, appliance housings, and aerospace bulkheads require multiple forming, piercing, and trimming stations within a single tool. As the part moves through the die, the tonnage requirements shift across the bed. A four-point setup provides the necessary support footprint to handle these complex, multi-station operations without sacrificing precision.
To successfully run large progressive dies, facilities must ensure the press meets specific geometric criteria:
The slide must maintain parallelism within 0.002 inches per foot of bed length under full load.
The bolster plate must feature adequate thickness to resist bowing under the center stations of the die.
The uprights must provide enough clearance for scrap shedding and automated part ejection.
The shut height must accommodate the tallest die in the facility's inventory while allowing room for future tool modifications.
Not all stamped parts are perfectly symmetrical. Asymmetrical drawing, blanking, or piercing operations naturally shift the center of tonnage away from the physical center of the press bed. For example, stamping a car door inner panel requires deep drawing on one end and shallow trimming on the other. This creates a severe eccentric load. If you run this die in a two-point press, the machine will struggle to maintain parallelism. Four-point suspension counteracts these eccentric loads mechanically. The four corner connections resist the uneven upward forces, forcing the slide to descend perfectly flat. Maintaining BDC accuracy across the entire bed ensures that asymmetrical parts form correctly without wrinkling, tearing, or requiring secondary flattening operations.
Material science heavily influences press selection. Stamping Advanced High-Strength Steels (AHSS), Dual Phase (DP) steels, and aerospace-grade aluminum alloys introduces extreme challenges. These materials require significantly higher tonnage to yield and form. Furthermore, they exhibit severe springback tendencies. Controlling springback requires applying high tonnage distributed evenly over a wide area at the bottom of the stroke. Additionally, blanking high-tensile materials generates massive snap-through forces. When the material fractures, the sudden release of stored energy sends a shockwave through the press, known as reverse tonnage. The sheer mass, rigidity, and uniform force application of a four-point mechanical press are required to absorb this shock. Lighter machines will tear themselves apart under the stress of continuous AHSS blanking.
Material Yield Strength vs. Press Requirements |
|||
Material Type |
Typical Yield Strength (MPa) |
Reverse Tonnage Risk |
Recommended Press Configuration |
|---|---|---|---|
Mild Steel (CQ/DQ) |
150 - 250 |
Low |
Two-Point or Four-Point |
High-Strength Low-Alloy (HSLA) |
300 - 550 |
Moderate |
Four-Point (for large beds) |
Advanced High-Strength Steel (AHSS) |
600 - 900+ |
High |
Four-Point (Mandatory) |
Martensitic Steels |
900 - 1500+ |
Extreme |
Four-Point with Hydraulic Dampers |
Four-point mechanical presses commonly use 8-point, full-length slide guiding systems to maintain accurate ram alignment and minimize lateral movement. Proper slide guidance reduces deflection, improves stamping precision, and prevents uneven die wear. Low deflection and consistent alignment help reduce burrs, material defects, and maintenance requirements during high-volume production.
Crankshaft drives are commonly used for high-speed blanking and shorter-stroke operations, while eccentric gear drives are often preferred for large presses requiring longer strokes and substantial forming energy. Both configurations offer different force and speed characteristics. Selecting the appropriate drive system improves forming performance, production efficiency, and equipment reliability.
Automated stamping systems integrate coil feeders, robotic handling, and transfer mechanisms to improve productivity and reduce manual operations. Four-point presses with suitable side openings and compatible control systems support efficient material movement between die stations. Accurate synchronization between press motion and automation equipment helps prevent collisions, reduce downtime, and maintain consistent production.
Energy-efficient stamping presses use high-efficiency motors, optimized drive systems, and suitable speed controls to reduce electricity consumption. Variable frequency drives (VFDs) can improve operating flexibility in compatible configurations, while regenerative systems may recover energy during deceleration. Evaluating power consumption and motor performance helps reduce operating costs and improve long-term efficiency.
New four-point mechanical presses offer modern frame designs, automation compatibility, and manufacturer warranties but require higher initial investment. Rebuilt presses can reduce acquisition costs by upgrading existing frames, controls, and mechanical components. Buyers should compare equipment condition, precision requirements, safety compliance, maintenance costs, and expected service life before making a decision.

High-precision four-point presses help improve return on investment (ROI) by maintaining consistent slide alignment, reducing scrap, and minimizing tooling wear. Better stamping accuracy can also reduce secondary finishing operations and unplanned downtime. These long-term savings help offset higher equipment costs while supporting stable, high-volume manufacturing.
Comparison of Press Capabilities and Production Impact |
||
Feature / Capability |
Two-Point Mechanical Press |
Four-Point Mechanical Press |
|---|---|---|
Suspension Points |
Two (Center-Left, Center-Right) |
Four (Corner-mounted) |
Off-Center Load Capacity |
Low to Moderate |
Exceptionally High |
Slide Tipping Risk |
High (with asymmetrical dies) |
Virtually Eliminated |
Ideal Bed Size |
Under 120 inches |
120 inches to 300+ inches |
Tooling Wear Rate |
Accelerated under eccentric loads |
Minimized due to strict parallelism |
Best Application |
Symmetrical blanking, smaller progressive dies |
Large body panels, AHSS, large transfer dies |
The initial purchase is only the beginning of the OEM relationship. Emphasize the importance of robust aftermarket support and accessible service networks. When a heavy-tonnage press goes down, it halts the entire production schedule. You need domestic or highly accessible OEM service technicians who can deploy immediately. Evaluate the vendor's mean time to repair (MTTR) metrics and their ability to provide remote diagnostics. A manufacturer with a strong regional service presence prevents minor electrical faults from escalating into catastrophic, multi-week downtime events.
Off-the-shelf solutions rarely fit complex stamping requirements perfectly. Evaluate the manufacturer's ability to customize the machine to your specific product lines. Can they engineer custom stroke lengths to accommodate deep-drawn parts? Can they modify shut heights to accept your existing die inventory? The OEM must demonstrate the engineering capability to modify window sizes, bolster plate machining, and automation integration points. A willingness to engineer the press around your specific transfer system ensures a smooth installation and immediate production efficiency.
Supply chain reliability directly impacts press uptime. Discuss the risk of proprietary components with potential vendors. If a manufacturer relies heavily on obscure, proprietary electronics or custom-machined wear parts, you face severe risks. Demand guaranteed lead times for critical replacement parts. You must know exactly how long it takes to procure replacement clutch/brake assemblies, bronze bushings, and drive gears. OEMs that utilize standardized, commercially available components for pneumatics, hydraulics, and controls offer a much safer long-term investment.
Calculate the exact center of tonnage, required bed area, and snap-through forces for your most demanding die.
Request a finite element analysis (FEA) of the proposed press frame under your specific load conditions from potential manufacturers.
Conduct a comprehensive facility audit to determine soil load-bearing capacity and foundation readiness.
Quantify the hidden costs of die maintenance caused by slide tipping in your current equipment to justify the capital expenditure.
A: The primary difference lies in the number of connections between the drive mechanism and the slide. A four-point press utilizes four corner connections, providing superior ability to handle off-center loads and maintain strict slide parallelism across massive bed areas compared to a two-point design.
A: Applications requiring large bed areas and handling severe off-center loads strictly require this equipment. This includes stamping automotive body panels, large appliance manufacturing, HVAC components, and running complex multi-station progressive or transfer dies.
A: Eccentric, off-center loads cause slide tipping or cocking in single or two-point presses. This deflection damages die guide pins and produces out-of-tolerance parts. The four-corner support of a four-point press resists these uneven forces, preventing die damage and maintaining precision.
A: While four-point mechanical presses can start around 400 tons for specialized applications, they are most common and critical in the heavy-duty range, typically spanning from 800 tons up to 3,000+ tons.
A: By maintaining rigid slide parallelism, four-point presses prevent uneven punch wear and die shearing. This stability significantly extends the time between required tool sharpenings, reducing tool room labor and lowering overall tooling maintenance costs.
A: Installing these massive machines requires engineered concrete foundation pits. Facilities must conduct soil load-bearing tests and install deep, heavily reinforced concrete bases, often incorporating vibration isolation pads to absorb dynamic shock and protect the surrounding factory floor.


