
Views: 0 Author: Site Editor Publish Time: 2026-10-12 Origin: Site


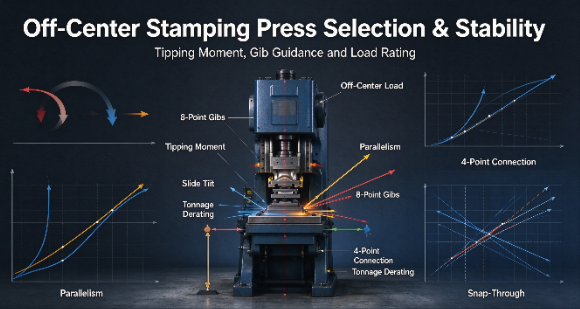
Perfectly centered stamping operations rarely exist on the shop floor. Heavy forming or blanking stations naturally fall toward the edges of progressive dies. These severe Off-Center Stamping Loads actively destroy standard equipment. They cause premature die wear, break tie rods, and lead to catastrophic slide tipping. Standard tonnage ratings assume you apply the load dead-center. Procurement teams often specify equipment based solely on total tonnage. They fail to account for the tipping moments generated by asymmetric part geometries. This oversight results in extensive downtime, severe safety hazards, and frequent mechanical rebuilds.
You need a technical framework to evaluate and specify a press for off-center load conditions. This guide breaks down the exact requirements for frame rigidity, connection points, drive types, gibbing architecture, and tonnage derating. You will learn how to match mechanical capabilities to your most extreme progressive die layouts, ensuring long-term stability and precision.
Frame Architecture is Non-Negotiable: Gap-frame (C-frame) presses are structurally unsuited for severe off-center loads; straight-side presses are mandatory for maintaining parallelism under asymmetric stress.
Connection Points Dictate Stability: A 2-point or 4-point press distributes force across the slide, actively resisting the tipping moment that would destroy a single-point press.
Gibbing Precision is Critical: 8-point, full-length gibs are required to constrain slide movement and absorb lateral forces generated by off-center stamping loads.
Drive Selection Matters: Choosing between mechanical, hydraulic, and servo drives must be dictated by the specific characteristics of the stamping process to mitigate snap-through shock.
Tonnage Must Be Derated: Press capacity drops significantly as the load moves away from the center line; calculating the reverse tonnage and tipping moment is a mandatory step in press selection.
Table of Contents
Off-center loading occurs when forming forces act away from the press slide's centerline, creating uneven stress during stamping. This can cause slide tilting, tooling misalignment, and dimensional defects. Successful operation requires sufficient frame rigidity, stable slide guidance, and consistent slide-to-bed parallelism under asymmetric loads.
Off-center loading damage often appears as uneven gib wear, scored slide guides, abnormal vibration, or tie-rod deformation. These warning signs may indicate excessive lateral forces or poor load distribution. Regular inspections of guide clearances, frame condition, and press alignment help detect problems early and prevent costly equipment failures.
Slide tipping occurs when uneven forming forces generate a twisting moment that disrupts slide-to-bed parallelism. This misalignment can cause punches to enter dies at an angle, resulting in excessive burrs, accelerated tooling wear, and inconsistent part dimensions. Rigid press frames and precision guiding systems help control deflection and maintain stamping accuracy.
Snap-through, also known as reverse tonnage, occurs when stored energy is suddenly released during material fracture. Under off-center loading, this shock can create uneven vibration and additional stress on press components. Proper frame rigidity, suitable drive configurations, and shock-control systems help reduce fatigue damage and protect stamping equipment.
Evaluating press specifications requires calculating the exact tipping moment generated by your dies. You calculate the tipping moment using a straightforward formula: Force multiplied by Distance from Center. You must establish this baseline metric before reviewing any press manufacturer's load curves.
Die Station Force (Tons) | Distance from Centerline (Inches) | Calculated Tipping Moment (Inch-Tons) | Impact on Press Slide |
|---|---|---|---|
50 | 10 | 500 | Minimal. Handled by standard 2-point presses. |
150 | 15 | 2,250 | Moderate. Requires tight 8-point gibbing. |
300 | 24 | 7,200 | Severe. Demands 4-point straight-side architecture. |
Knowing your maximum tipping moment allows you to specify a machine capable of handling the exact rotational forces your production demands. Never guess these numbers; extract them directly from your tooling engineering data.
Press frame design directly affects structural rigidity, load distribution, and resistance to off-center forces. The two main configurations are C-frame presses and straight-side presses. Selecting the appropriate structure depends on stamping tonnage, die dimensions, and precision requirements.
C-frame presses provide convenient three-sided access but are more susceptible to angular deflection under heavy or off-center loads. Excessive frame movement can affect slide parallelism, causing tooling misalignment and premature wear. They are generally better suited for lighter stamping operations within their rated load limits.
Straight-side presses feature a closed-frame structure that provides greater rigidity and more uniform load distribution. Reinforced uprights help resist tipping moments and minimize slide deflection during asymmetric stamping. This design improves tooling alignment, dimensional accuracy, and equipment reliability in heavy-duty applications.
Tie-rod frames use preloaded steel rods to connect the crown, uprights, and bed, providing structural stability under heavy stamping loads. Solid welded frames offer compact construction and reliable performance for suitable applications. The best choice depends on required tonnage, frame stiffness, load distribution, and maintenance considerations.
Rebuilding an existing press can be cost-effective when the frame remains structurally sound. Upgrading slide guides, overload protection, and control systems may improve performance. However, presses with severe structural damage or insufficient off-center load capacity may require replacement. Engineers should compare repair costs, frame condition, and long-term production requirements before deciding.

Evaluating a press requires breaking down specific mechanical components and mapping them to production outcomes. You cannot rely on top-level tonnage alone. You must scrutinize the connection points, the guiding architecture, and the drive gear placement. Each of these components plays a direct role in capturing and neutralizing the tipping forces generated by your dies.
The number of connection points between the drive shaft and the slide dictates how force distributes across the die space. This specification makes or breaks off-center performance.
Connection Type | Force Distribution | Suitability for Off-Center Loads |
|---|---|---|
1-Point | Dead center only. | Zero resistance to tipping. Disqualify entirely. |
2-Point | Left-to-Right (X-axis). | Excellent for standard progressive dies with lateral shifts. |
4-Point | Four corners (X and Y axes). | The gold standard. Handles severe front-to-back and left-to-right forces. |
Always match the connection type to the physical layout of your heaviest dies. A 4-point connection provides maximum insurance against slide tipping.
8-point adjustable gibs provide improved slide guidance and stability under off-center loads. Compared with standard 4-point systems, they offer additional support to reduce lateral movement and slide tilting. Proper gib materials, lubrication, and manufacturer-specified clearances help maintain ram alignment and extend tooling life.
Drive gear placement affects load distribution and slide stability. Center-drive systems may experience greater shaft torsion under uneven loading, while twin-end drive configurations distribute driving forces more evenly. Proper drive design helps reduce twisting, improve slide synchronization, and maintain stamping accuracy.
Press drive selection should match the forming process, production speed, and off-center loading requirements. Mechanical, hydraulic, and servo systems offer different force delivery and motion control capabilities. Selecting the appropriate drive helps improve forming accuracy, minimize equipment stress, and maintain production efficiency.
Drive Type | Key Advantages | Suitable Applications |
|---|---|---|
Mechanical | High speed and repeatable operation | Progressive blanking and punching |
Hydraulic | Controllable force and adjustable forming speed | Deep drawing and complex forming |
Servo | Programmable motion and improved speed control | Precision stamping and complex forming |
All three drive types require appropriate press rigidity and off-center load capacity to prevent slide tilting and tooling damage.
Tonnage derating accounts for reduced allowable press capacity under off-center loading. Engineers should use the manufacturer's off-center load curves to compare applied force, load position, and permissible capacity. For example, a 500-ton press may have a substantially lower allowable load when the force acts away from the centerline. Proper verification helps prevent localized overload and equipment damage.
Bed and slide rigidity directly influence stamping accuracy under asymmetric loads. Excessive deflection causes uneven die clearance, dimensional variations, and premature tooling wear. Selecting a press with suitable stiffness and manufacturer-verified deflection limits helps maintain consistent part quality and improve die service life.
Managing off-center stamping loads requires coordinated press selection, die design, safety systems, and maintenance planning. Even a high-rigidity press can experience premature wear if tooling loads exceed its operating limits. Evaluating the complete stamping system helps reduce mechanical stress and improve long-term reliability.
Hydraulic overload protection (HOLP) helps protect mechanical presses from excessive loading by detecting overload conditions and activating the appropriate protection mechanism. Multi-point protection is particularly important for asymmetric stamping operations. Proper overload settings and safety controls help reduce equipment damage and operational risks.
Die load balancing helps reduce excessive tipping moments during off-center stamping. Engineers may optimize station placement or use suitable pressure pads, nitrogen springs, and other die components to improve load distribution. These measures should be engineered carefully to avoid introducing unnecessary force or additional tooling stress.
Regular maintenance is essential for presses operating under repeated off-center loads. Key inspections include gib clearance, tie-rod tension, lubrication performance, and bolster plate condition. Monitoring these components helps identify uneven wear, prevent alignment problems, and maintain reliable stamping performance.
Multi-channel tonnage monitoring systems measure load distribution across different press connection points during operation. Strain gauges detect uneven forces and potential overload conditions, allowing operators to identify abnormal loading patterns. Properly configured monitoring and stop controls help protect tooling, reduce downtime, and improve production consistency.
Selecting a press for off-center load conditions requires a fundamental shift in procurement strategy. You must prioritize structural rigidity, slide guiding, and appropriate drive technology over raw, center-rated tonnage. A machine that looks adequate on paper will tear itself apart if it lacks the specific geometry required to neutralize tipping moments. The ideal specification for severe asymmetric work is a straight-side press featuring a 2-point or 4-point connection, a twin-end drive system, and 8-point gibbing.
Map out your most extreme progressive die layouts and identify the heaviest forming stations.
Calculate the maximum tipping moments for each die using the force-times-distance formula.
Present these specific calculations and die maps to press manufacturers during the RFQ process.
Demand certified off-center load curves from vendors to prove their machines can handle your specific asymmetric requirements.
A: There is no universal maximum. You must consult the manufacturer's specific off-center load curve for the exact machine. The allowable load varies drastically based on the connection type, frame rigidity, and the exact distance the load is applied from the press centerline.
A: While minor off-center loads are possible on smaller parts, C-frames are highly prone to angular deflection (yaw) due to their open-throat design. They lack the front uprights needed to resist torque and are not recommended for severe asymmetric work.
A: Extra-long 8-point gibs capture the slide at eight distinct locations along its full stroke. They constrain the slide in all lateral directions, actively absorbing the moment arm forces generated by the off-center load and transferring that stress into the rigid press uprights.
A: Exceeding the off-center rating causes immediate and severe mechanical failure. Consequences include broken pitman connections, deeply scored gibs, snapped tie rods, cracked press frames, ruined die alignment, and severe safety hazards for operators.
A: Reverse tonnage (snap-through) occurs when the punch breaks through the metal. When this happens off-center, it creates violent, asymmetric shockwaves. This uneven release of energy compounds the mechanical stress, twisting the slide and fatiguing the press frame.
A: A 4-point press is superior for handling front-to-back off-center loads due to its four corner connections. However, a 2-point press is often highly effective and sufficient for standard progressive dies where the off-center load shifts primarily left-to-right.
A: Yes. Servo presses feature programmable stroke profiles. You can program the ram to slow down just milliseconds before material breakthrough. This drastically reduces the asymmetric snap-through shock that typically damages press frames during heavy off-center blanking.


